
Preface
A user uses a batch of bearing steel wire rod GCr15-Y of 18mm specification of Nangang, and the middle is annealed in a roller-bottom continuous annealing furnace. The continuous annealing furnace is a nitrogen protection vacuum air-locking roller-bottom spheroidizing annealing furnace.
The process flow of spheroidizing annealing is as follows: incoming material inspection → loading onto the feeding table → entering the front vacuum chamber (pumping air and filling nitrogen) → entering the preheating zone, heating zone, heat preservation zone, fast cooling zone, isothermal zone, slow cooling zone, and free cooling zone from the vacuum chamber (heating up to 795 ℃, heat preservation for 7h, fast cooling to 720 ℃, heat preservation for 5h, and cooling down to 650 ℃ at 20 ℃/h) → entering the cold water bin → entering the rear vacuum chamber → discharging table.
After raw material inspection → acid pickling → phosphorus saponification → light drawing of a layer of 30 wires → blanking and cold upsetting into a blank ferrule, the naked eye can see that there is cracking on the ferrule end face, the cracking ratio is between 10% and 15%, the cracking position is discontinuous, and the crack position is perpendicular to the rolling extension direction along the radial direction of the wire rod, as shown in Figure 1.

Figure 1
The user feedback that the spheroidizing annealing, wire drawing and cold heading process are normal, and only the cracking rate of the cold heading ring of this batch of bearing steel wire rod exceeds 10%, which has a great relationship with the original wire rod.
Wire rod production process: blank shot blasting Spot grinding treatment → walking beam furnace heating (preheating section 700~750 ℃, heating section 1 930~960 ℃, heating section 2 1130~1160 ℃, soaking section 1200~1240 ℃, heating section 2 and soaking section high temperature section time 60~100min.) → high-pressure water descaling → rough rolling → intermediate rolling → pre-finishing rolling → water cooling in zone 1 → finishing rolling → water cooling in zone 2 → reducing sizing → water cooling in zone 3 → wire drawing → air cooling in Stelmo → coiling → finishing → baling → weighing → warehousing.
1 Analysis of cracked ferrule sample
Four samples are randomly taken from the cracked ferrule samples, two of which are used for high and low magnification inspection and hardness analysis, and the other two ferrules are used for carbide inhomogeneity and fracture inspection and grain size analysis.
1.1 Macroscopic inspection
One ferrule cracking sample is selected at random and observed under the stereomicroscope. The macroscopic morphology of ferrule cracking is shown in Figure 2.

Figure 2
1.2 Macroscopic inspection
One of the ferrules was etched in hot hydrochloric acid (concentration 31%, temperature 70~80 ℃) for 8~10min and then taken out. Macroscopic examination showed that there were multiple cracks on both sides of the ferrule, as shown in Fig. 3a on the front and Fig. 3b on the back.
Figure 3
Grind 2~3mm off one end of the other ferrule sample, cut a part along the longitudinal section, and take it out after etching in hot hydrochloric acid (concentration 31%, temperature 70~80 ℃) for 8~10 minutes. According to the national standard/GBT18254, the central porosity and general porosity are evaluated as Grade 1.0, and no shrinkage defects are found. The appearance is shown in Figure 4. Therefore, the end face cracking of the ferrule has nothing to do with the macrostructure of the raw material.

Figure 4
1.3 Macroscopic inspection
1.3.1 Annealed state inspection of ferrule crack
After taking samples from the two cracks on the right side of the end face in Fig. 2 and grinding, observe the longitudinal section under the microscope, and no inclusions and oxides are found in and around the cracked crack. Observe after corrosion, the microstructure of both sides of the crack is consistent with that of the matrix, which is spheroidal pearlite distributed on the ferrite matrix, and no decarburization is found at the edge of the sample and the crack, as shown in Fig. 5, The microstructure of both sides of the crack on the cross section is consistent with that of the matrix, which is spheroidal pearlite distributed on the ferrite matrix, as shown in Figure 5.

Figure 5
1.3.2 Uneven carbide inspection
After a ferrule is quenched and tempered, the non-uniformity of the carbide in the longitudinal section is examined under the microscope. It is found that the banded and reticulated morphology is as shown in Figure 6. According to the national standard GB/T18254, the ferrule is rated as banded and reticulated 1.5, and no carbide precipitation is found, which meets the requirements of the national standard. Therefore, the end face cracking of the ferrule has nothing to do with the uniformity of carbide in the raw material.

Figure 6
1.4 Brinell hardness test of ferrule
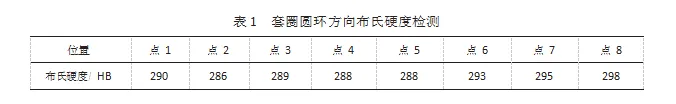
Brinell hardness test was carried out randomly along the ring direction of the ferrule. The hardness was relatively uniform, with an average hardness of 290.8HB. No obvious high or low points were found. The test data are shown in Table 1.
1.5 Ferrule fracture inspection
After quenching treatment, a ferrule is broken at one time. The longitudinal section fracture structure of the ferrule is examined by stereomicroscope. There are many bright surfaces on the macro fracture surface. Each bright surface is a grain interface. The fracture path extends along the grain boundary in different directions, which is a typical intergranular brittle fracture. The morphology is shown in Figure 7.
According to the principle of minimum fracture energy consumption, the crack propagation path always extends along the surface with the weakest atomic bonding force, which largely depends on the state and nature of the crystal interface. The grain boundary strength is not necessarily the lowest, but if the metal has some metallurgical factors that weaken the grain boundary (for example, the billet is overheated or burnt), the metal will undergo intergranular brittle fracture.

Figure 7
1.6 Inspection of austenite grain size of ferrule
The grain size of the longitudinal section sample of the prepared fracture was examined under the microscope, and it was found that the grain size of the outer wall of the ferrule was significantly coarser than that of the base, and the morphology was as shown in Figure 8. Therefore, it is speculated that the fracture specimen is related to the original wire rod heating process, that is, the local overheating of the billet during the heating process.

Figure 8
2. Defective wire rod process tracing and production process improvement of bearing steel wire rod for ferrule
Through the detection of the macrostructure, hardness, carbide, fracture and grain size of the cracked sample, the macrostructure, carbide uniformity and surface hardness are normal, while the fracture has overheated structure, and the grain size of the outer wall of the ferrule is significantly coarser than that of the base. It is speculated that this is related to the local overheating of the original wire rod heating process, that is, the billet during the heating process.
Tracing the heating process of the cracked batch of wire rods, the rolling batch number C60199901, a total of 47 billets, had been put into the furnace at the time of changing the specification, only 10 steps away from the furnace head, the preheating section 701~715 ℃, the heating section 952~959 ℃, the heating section 1148~1156 ℃, meeting the process requirements, while the soaking section 1245~1248 ℃, the heating section II and the soaking section high temperature section 126 minutes, exceeding the upper limit of the process specification.
In order to quickly solve the cracking of bearing steel wire rod cold heading ring, the heating process of bearing steel wire rod is optimized:
The feeding position of bearing steel billet is optimized. During roll change, the bearing steel blank used to make the collar is not allowed to enter the heating section directly. The first blank is at least 48 steps away from the tapping position of the furnace head, as shown in Figure 9. When the transition steel grade is not enough, it is necessary to leave enough step space, and use the roll change time to complete the empty step space according to the normal tapping rhythm, so as to prevent the bearing steel billet from staying in the furnace heating section for a long time and causing local overheating defects.

Figure 9
The heating time of the bearing steel blank is optimized, and the residence time of the bearing steel blank in the high temperature section after entering the second heating section and soaking section is controlled to not exceed 100min.
The heating temperature and tapping temperature of bearing steel billets are optimized. In order to avoid local overheating of bearing steel billets in the high temperature section of the furnace, the heating temperature shall be strictly controlled. The maximum heating temperature of the heating section and soaking section shall not exceed 1220 ℃, and the temperature of red steel after descaling shall not exceed 1130 ℃.
3 Implementation effect of process improvement
After the process improvement, the bearing steel wire rod GCr15-Y with heat number 16706548, a total of 45 billets, was produced again for a user to produce 18mm ring. When changing the size of 18mm, only 24 pieces of this furnace number blank are put into the furnace, and the roll change time is 50min. After the roll change, the production process is relatively smooth. The residence time of the high temperature section of the heating section II and soaking section is 68min, the temperature of the heating section II is 1135 ℃, the temperature of the soaking section is 1212 ℃, and the temperature of the red steel after descaling is 1122 ℃.
Compare the austenite grain size of this batch of wire rod sample with that of the wire rod with overheating defects in the past. It is found that the edge grain size of the wire rod with overheating defects is obviously coarse, while this time the wire rod grain size is relatively uniform and fine, as shown in Figure 10.

Figure 10
The user did not complain about the quality problems after using this batch of wire rods. According to the user's feedback, the cracking rate in the process of cold heading ferrules decreased significantly, from more than 10% to less than 0.5%.
4 Conclusion
The cracking of the bearing steel wire rod cold heading collar is related to the original wire rod heating process, that is, the local overheating of the steel billet during the heating process. When arranging the production plan of the bearing steel wire rod used for the collar, try to avoid the bearing steel billet directly entering the heating section when changing the roll. If it is really unavoidable, the steel grade should be transferred according to the row or the corresponding step should be vacated.
The heating temperature and heating time shall be strictly controlled. The residence time of the high temperature section after the billet enters the second heating section and soaking section shall not exceed 100min, the maximum heating temperature shall not exceed 1220 ℃, and the temperature of the red steel after descaling shall not exceed 1130 ℃.
The improved process has been used to continuously produce multiple batches, and there has been no batch cracking quality complaint.
More about WBM Carbide Cold Heading Dies:
WBM can produce different types and sizes Steel Ball Dies with quality assurance, include: carbide steel ball cold heading dies, Steel ball cold heading dies for national.
Materials: tungsten carbide or mold steel
Main parts for cold heading process: Quill (cut off die), cutter (cut off blade), punch, taper dies. No matter your material is case harden steel or through harden steel, our full set dies can run in a good lifetime.
High precision dies produced according to your drawing. And we can also provide tools design service according to your roller headers.
