Some bearing factories urgently need to improve their current cold heading machines in order to improve the accuracy of their parts. Some bearing factories want to change the steel ball cold heading machine to a roller cold heading machine based on changes in market demand for ball bearings and roller bearings, while others want to change the roller cold heading machine to a steel ball cold heading machine. To transform, it is necessary to first understand the workpiece deformation process and the working principle of the machine.
The upsetting process of steel balls involves first firmly clamping the material section between the concave and convex molds using an elastic punch (Figure 1). After the cutting plate or clamp exits the upsetting area, the upsetting process is carried out under the action of the slider. The distance L between the two molds can completely ensure that the blade or clamp can safely exit the forging area. Elastic pliers or knife hooks also do not pull the material off. If the machine is not modified and only the steel ball mold is replaced with a roller mold to upset the rollers, it is not feasible. Because when the concave and convex molds clamp the material (Figure 2), the distance L between the concave and convex molds is too small, and the blade or clamp cannot move forward or backward. If we arrange the space for the gripper to move in and out according to the movement time (Figure 3), the material segment will float between the concave and convex molds. Due to the material deviation, the upset workpiece will overlap, and when the gripper or knife hook exits, the material will be pulled off, resulting in a large amount of waste. The current roller cold heading machines all have a material section insertion device, which is used to insert the material into the mold cavity and exit the forging area before the punch enters the forward forging. The exercise cycle time is different from that of a steel ball cold heading machine. To convert a steel ball cold heading machine into a roller cold heading machine, in addition to adding a driving device, it is also necessary to change the motion cycle time of each part of the machine. This method is relatively complex.
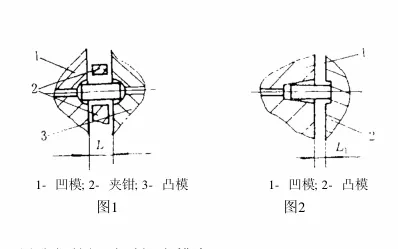
1-concave mold; 2-clamp;3-convex mold; 1- concave mold;
Figure 1 2-convex mold;
Figure 2
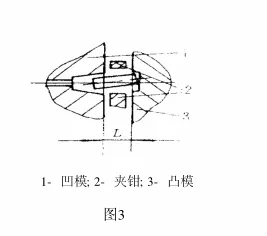
1-concave mold; 2-clamp;3-convex mold;
Figure 3
The steel ball cold heading machine is simple, and its improvement method is to first remove the punch holder on the slider and install an adjustable punch bracket on the bed between the slider and the concave mold seat. The punch slides in the bracket to complete the forging (Figure 4). The movement of the punch is controlled by the slider and cam. When the punch moves to a distance of S' from the concave die (which is larger than the width of the clamp and smaller than the length of the material section), it stops. After the clamp exits the upsetting zone, the punch undergoes upsetting under the action of the slider. The precision of this structure's parts is not affected by the slider motion accuracy, which is greatly improved compared to before the transformation, and the accuracy remains unchanged after adjustment (we improved three Z3210 steel ball cold heading machines using this technology for Luoyang Bearing Factory, and the pressure deviation of the parts is within 0.025mm). If using this machine to upset rollers, the following two modification measures need to be taken: (1) the spring inside the concave mold changes position to keep the push needle at the front end face of the concave mold (Figure 5). If the mold cavity cannot be arranged, a method can also be found on the push rod. The purpose is to catch the material section, otherwise the situation shown in Figure 3 will occur. (2) There must be a clamp opening (Figure 6) and hook opening (Figure 7) mechanism, otherwise the material section will be tilted or pulled off, resulting in a large amount of waste. The transmission mode of the clamp opening mechanism is arranged according to the actual situation of different models of machines (if using a roller cold heading machine to upset steel balls, a convex die needs to be added for pushing out).
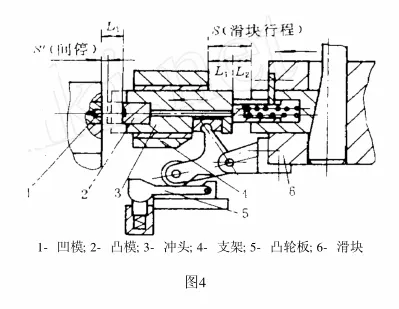
1- concave mold; 2-convex mold; 3-punch; 4-bracket; 5- Cam plate; 6-Slider
Figure 4
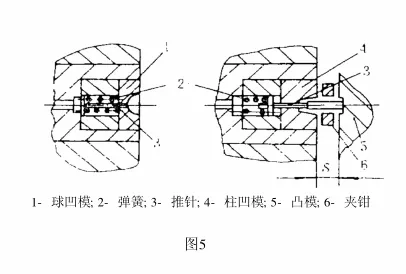
1- Ball concave mold; 2- Spring; 3- Pushing needle; 4-column concave mold; 5-convex mold; 6-clamp
Figure 5
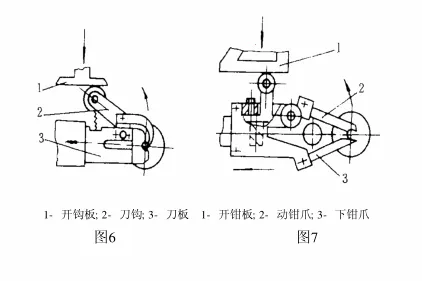
1- Hook opening plate; 2- Knife hook; 3-Knife plate
Figure 6
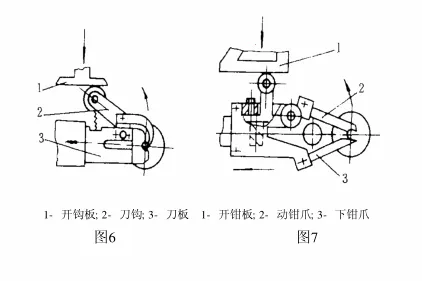
1. Plate opening pliers; 2- Moving pliers; 3- Lower jaw
Figure 7
More about WBM Modler End Face Grinder Tools:
Weichuang now have the ability to supply full set tooling for Modler taper roller grinding line. Our tooling are well fitted in customer modler centerless grinder and modler end face grinder. And help customer produce high precision rollers with low cost.
https://www.bearingroller.com/tools/modler-end-face-grinder-tools.html