
Abstract
The present invention provides a warm forging blank for cold finishing of a three pin axle fork precision forging. The warm forging blank comprises a handle and a bowl shaped head, and the inner cavity surface of the head is distributed with multiple spherical paths in a circumferential direction, with spherical surfaces between adjacent spherical paths; The cross-section at the bottom of the inner cavity of the head is the bowl bottom reference surface of the head. The outer surface above the bowl bottom reference surface of the head is divided into two parts. The first outer surface corresponds to the ball path inside the head, and the second outer surface corresponds to the spherical surface inside the head. The first outer surface has a draft slope extending upward from the bowl bottom reference surface of the head, and the axial tangent line corresponding to the draft slope forms an angle with the axis of the warm forging. The second outer surface has a draft slope extending upward from the bowl bottom reference surface of the head, and the axial tangent line corresponding to the draft slope forms an angle with the axis of the warm forging. The first and second angles are not equal. The present invention avoids the occurrence of cracks at the bottom of the mold cavity of the head due to excessive refrigerant pressure, and improves the production quality of the three pin axle fork.
Description
Warm forging blanks for cold finishing of three pin fork precision forgings
technical field
The present invention relates to the production technology field of three pin axle forks, particularly to a warm forging blank for cold finishing of three pin axle fork precision forgings.
Background technology
The transmission shaft of a car is the direct driving component for the rotation of the wheels. When the car is running, the torque output by the engine is transmitted to the transmission shaft through multi-stage transmission and the driver, and then transmitted to the wheels by the transmission shaft, pushing the car forward or backward. It is an important component for transmitting torque in the car. The three pin axle fork is the main load-bearing component of the automobile transmission shaft, and its working condition is extremely complex. Its performance directly affects the safety and reliability of the automobile transmission.
Three pin axle forks are generally produced using a combined warm and cold forming process. The typical process of this process (taking the precision forging of a three pin axle fork with an automotive constant velocity universal joint as an example) includes: cutting → shot blasting → pre coating graphite → induction heating → forward extrusion handle → upsetting the pre formed head cavity → reverse extrusion forming of the warm forging blank → temperature controlled cooling → shot blasting → saponification → cold finishing (reduced diameter cold extrusion). The warm forging blank formed by reverse extrusion directly affects the subsequent cold finishing forming process. The warm forging blank used in existing cold finishing has a 6 ° draft slope with a height of about 5mm (shown as 4.739 ± 0.5 in Figure 1) starting from the bowl bottom reference surface A of the head, as shown in Figure 1. The 6 ° draft slope extends all the way to the head bottom plane B where the head and handle are connected, and the corresponding inner cavity diameter at the bowl bottom reference surface A of the head is D. In actual production, if the blank design of the three pin axle fork warm forging is improper, cracks may occur at the bottom of the mold cavity due to excessive cold extrusion pressure during cold finishing of the head cavity.
Therefore, a three pin axle fork warm forging blank suitable for cold finishing process is needed.
summary of the invention
In view of the shortcomings of the existing technology mentioned above, the purpose of the present invention is to provide a warm forging blank for cold finishing of a three pin axle fork precision forging, which is used to solve the problem of cracks easily occurring when the warm forging blank enters the cold finishing process in the existing technology.
In order to achieve the above objectives and other related objectives, the present invention provides a warm forging blank for cold finishing of a three pin axle fork precision forging. The warm forging blank comprises a handle and a bowl shaped head, and the inner cavity surface of the head is distributed with multiple ball paths in a circumferential direction, with ball surfaces between adjacent ball paths; The cross-section at the bottom of the inner cavity of the head is the bowl bottom reference surface of the head. The outer surface above the bowl bottom reference surface of the head is divided into two parts, one part is referred to as outer surface one and corresponds to the ball path inside the head, and the other part is referred to as outer surface two and corresponds to the spherical surface inside the head. The outer surface one has a draft slope one extending upward from the bowl bottom reference surface of the head, and the axial tangent line corresponding to draft slope one forms an angle one with the axis of the warm forging. The outer surface two has a draft slope two extending upward from the bowl bottom reference surface of the head, and the axial tangent line corresponding to draft slope two forms an angle two with the axis of the warm forging. Angle one and angle two are not equal.
Preferably, the cross-section where the handle is connected to the head is the bottom plane of the head, and the axial tangent line corresponding to the outer surface between the bottom plane of the head and the bowl bottom reference plane of the head is parallel to the axis of the warm forging.
Preferably, the axial height of the draft inclined plane one is 6-8mm; And the angle one is 13 ° to 15 °.
The preferred angle is 14 °.
Preferably, the axial height of the draft inclined surface two is 6-8mm; And the angle mentioned is between 8 ° and 10 °.
The preferred angle is 11 °.
Preferably, the surface one and the outer surface two are connected by a transition surface, which has a draft inclined surface three extending upward from the bowl bottom reference surface of the head. The axial tangent line corresponding to draft inclined surface three forms an angle three with the axis of the warm forging, and the angle three is 10 ° to 12 °.
Preferably, the height of the draft slope three is 6-8mm.
As described above, the warm forging blank used for cold finishing of the three pin axle fork precision forging of the present invention has the following beneficial effects: the outer surface of the head is divided into two parts, one for the ball path of the head cavity and the other for the spherical surface of the head cavity, and the two parts are designed differently to have different angles of draft angles, thereby reducing the cold extrusion pressure during the cold finishing process, avoiding excessive refrigerant pressure that may cause cracks at the bottom of the head cavity, and improving the production quality of the three pin axle fork.
Attached image description
Figure 1 shows a schematic diagram of a three pin axle fork warm forging blank in the prior art.
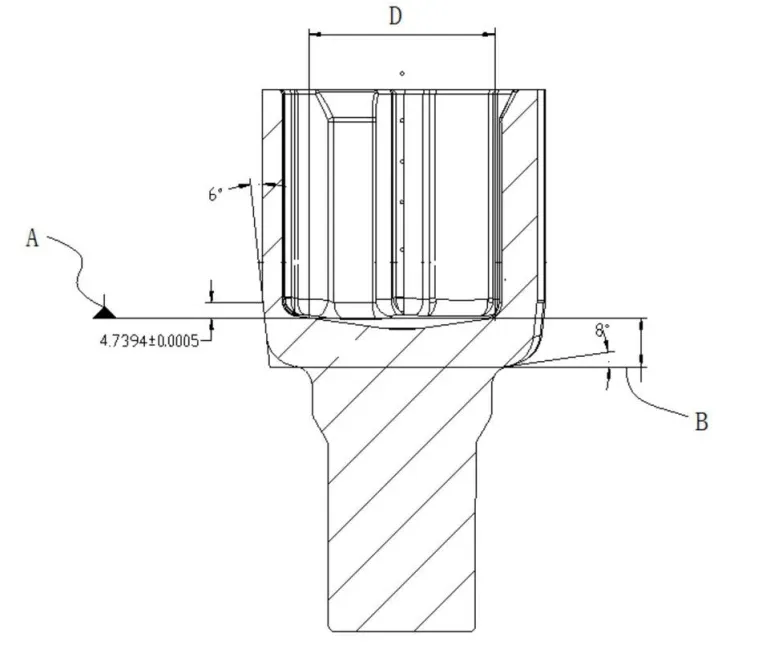
Figure 2 shows a schematic diagram of the three pin axle fork warm forging blank of the present invention.
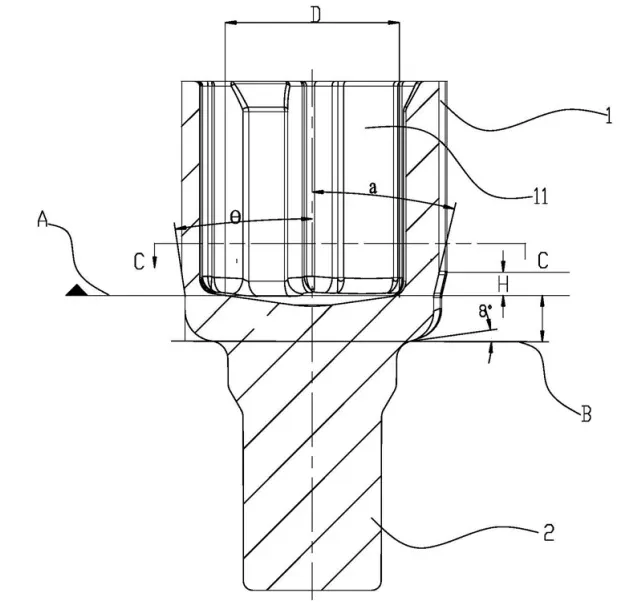
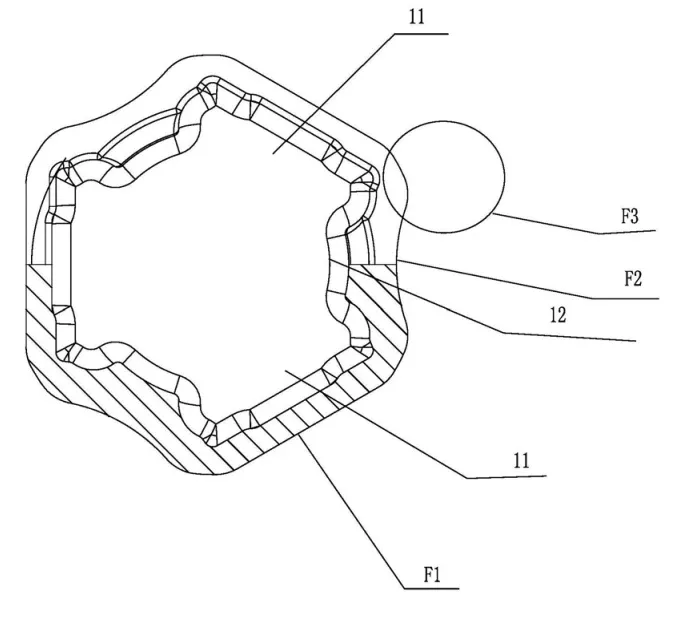
Figure 3 shows a cross-sectional view along the CC line in Figure 2.
Specific implementation method
The following specific embodiments illustrate the implementation of the present invention, and those familiar with this technology can easily understand other advantages and effects of the present invention from the content disclosed in this specification.
Please refer to Figures 1 to 3. It should be noted that the structures, proportions, sizes, etc. shown in the accompanying drawings of this specification are only for the purpose of cooperating with the content disclosed in the specification, for the understanding and reading of those familiar with this technology, and are not intended to limit the conditions under which the present invention can be implemented. Therefore, they do not have any substantive technical meaning. Any modification of the structure, change in the proportion relationship, or adjustment of the size should still fall within the scope of the technical content disclosed in the present invention, without affecting the efficacy and objectives that can be achieved by the present invention. Meanwhile, the terms used in this specification, such as "up", "down", "left", "right", "middle", and "one", are only for the sake of clarity in description and are not intended to limit the scope of the present invention. Any changes or adjustments in their relative relationships, without substantial changes in technical content, shall also be considered as the scope of the present invention.
As shown in Figures 2 and 3, the present invention provides a warm forging blank for cold finishing of a three pin axle fork precision forging. The warm forging blank comprises a handle portion 2 and a bowl shaped head portion 1. The inner cavity surface of the head portion 1 is distributed with multiple ball paths 11 in a circumferential direction, and the adjacent ball paths are spherical surfaces 12; The cross-section at the bottom of the inner cavity of the head is the bowl bottom reference surface A of the head. The outer surface above the bowl bottom reference surface A of the head is divided into two parts, one part is referred to as the outer surface F1 and corresponds to the raceway 11 inside the head, and the other part is referred to as the outer surface F2 and corresponds to the spherical surface 12 inside the head. The outer surface F1 has a draft inclined plane 1 extending upward from the bowl bottom reference surface A of the head, and the axial tangent line corresponding to the draft inclined plane 1 forms an angle of one θ with the axis of the warm forging. The outer surface F2 has a draft inclined plane 2 extending upward from the bowl bottom reference surface A of the head, and the draft inclined plane 2 corresponds to the draft inclined plane 2. The axial tangent of the forging forms an angle 2a with the axis of the warm forging, and the angle θ and angle 2a are not equal. The present invention divides the outer surface of the head into two parts, one for the ball path 11 inside the head cavity and the other for the spherical surface 12 inside the head cavity. Different designs are made for the two parts to have draft angles at different angles, in order to reduce the cold extrusion pressure during the cold finishing process, avoid excessive refrigerant pressure from causing cracks at the bottom of the head cavity, and improve the production quality of three pin fork precision forgings.
In order to better reduce the refrigerant pressure on the warm forging blank during the cold finishing process, in this embodiment, the cross-section at the connection between the handle 2 and the head 1 is the bottom plane B of the head. The axial tangent of the outer surface between the bottom plane B of the head and the bowl bottom reference plane A of the head is parallel to the axis of the warm forging, that is, the outer surface between the bottom plane B of the head and the bowl bottom reference plane A of the head has no slope and is cylindrical.
In order to avoid cracks during the cold finishing process, the axial height H of the draft inclined surface 1 in this embodiment is 6-8mm; And the angle θ is 13 ° to 15 °. The preferred axial height H of the draft inclined plane one is 7.5mm, and the angle one θ is 14 °. To avoid the occurrence of cracks during the cold finishing process, the axial height H of the draft angle 2 in this embodiment is 6-8mm; And the angle 2a is between 8 ° and 10 °. The preferred axial height H of the draft inclined plane 2 is 7.5mm, and the angle 2a is 11 °. This setting reduces the cross-sectional area of the bowl bottom reference plane A at the head, decreases the reduction rate of the cold finishing part section, and reduces the cold extrusion pressure.
In this embodiment, the outer surface F1 and the outer surface F2 are connected by a transition surface F3, as shown in Figure 3. The transition surface F3 has a draft inclined surface three extending upward from the bowl bottom reference surface A of the head. The axial tangent line corresponding to the draft inclined surface three forms an angle three with the axis of the warm forging, and the angle three is 10 ° to 12 °. The preferred height for the draft angle three is 6-8mm.
Based on the design of the warm forging blank used for cold finishing of the three pin axle fork mentioned above, simulated using the 3D forging forming simulation software DEOFORM, the maximum cold extrusion pressure load is 478 KN. Compared with the warm forging blank used for cold finishing of the three pin axle fork in the existing technology, the maximum cold extrusion pressure load is reduced by 13.5%, avoiding cracks at the bottom of the forging bowl during cold finishing and improving the service life of the forging.
In summary, the warm forging blank used for cold finishing of the three pin axle fork precision forging of the present invention divides the outer surface of the head into two parts, one for the ball path 11 of the head cavity and the other for the ball surface 12 of the head cavity. Different designs are made for the two parts to have different angles of draft angles, in order to reduce the cold extrusion pressure during the cold finishing process, avoid excessive refrigerant pressure from causing cracks at the bottom of the head cavity, and improve the production quality of the three pin axle fork. Therefore, the present invention effectively overcomes various shortcomings in the prior art and has high industrial utilization value.
The above embodiments are only illustrative of the principles and effects of the present invention, and are not intended to limit the present invention. Anyone familiar with this technology may modify or alter the above embodiments without departing from the spirit and scope of the present invention. Therefore, all equivalent modifications or changes made by those with ordinary knowledge in the relevant technical field without departing from the spirit and technical ideas disclosed in the present invention should still be covered by the claims of the present invention.
2024 December 3rd Week WBM Product Recommendation:
Rolling Dies:
As one of the professional tool manufacturer, provides rolling die with high hardness,fast delivery and good service.
https://www.bearingroller.com/tools/rolling-dies.html
