Abstract
A high-precision process for the convexity of cylindrical rollers and tapered rollers. A guide roller with two spiral rolling surfaces as conical surfaces is used, and the axis of the workpiece is inclined to the left or right at an angle α relative to its advancing direction B. The upper generatrix of the workpiece is parallel to the plane formed by the axis of the two guide rollers. Under the support and driving of the guide roller and the action of the oilstone group, the outer diameter of the workpiece can obtain a "logarithmic curve" convex shape, which has the characteristics of easy operation and stable processability. In addition, the design and manufacturing of the guide roller are simple, suitable for wide promotion.
Description
The present invention relates to a process for grinding, particularly a convex ultra precision process for cylindrical rollers, tapered rollers or similar objects.
The existing cylindrical roller convexity ultra precision technology uses ultra precision guide rollers without spiral ribs. In order for the processed cylindrical roller to move forward automatically, the two guide wheels must be inclined at a certain angle to each other in the vertical direction. Therefore, the design and manufacturing of this guide roller are quite complex. Some manufacturers have to introduce it from abroad, and the convexity exceeded by this method is semi convex or fully convex, which cannot achieve the logarithmic curve convexity that can withstand the load most; However, the ultra precision convexity of tapered rollers is a blank in China.
The purpose of the present invention is to provide a convex ultra precision process that enables cylindrical rollers, tapered rollers, or similar objects to achieve logarithmic curve like convexity in their outer diameters, with easy manufacturing and convenient operation of the device.
The technical solution of the present invention is a cylindrical roller and tapered roller convexity ultra precision process, which adopts a system composed of two cooperating guide rollers and an oilstone group. The workpiece rotates continuously in the direction B specified by the guide rollers while being supported and driven by the guide rollers. Under the action of the vibration frequency f and pressure P of the oilstone group, the outer diameter of the roller is processed using a centerless through ultra precision machining method to achieve convexity. Its special feature is that the axis lines of the two guide rollers are parallel, and the spiral groove rolling surface opened by them is a cone. One of the guide rollers is equipped with a spiral guard edge. The spiral groove rolling surface of the guide roller is matched with the outer surface of the workpiece, so that the axis of the workpiece is inclined to the left or right by an angle α relative to its advancing direction B, and the upper generatrix of the workpiece is parallel to the plane formed by the axis of the guide roller.
When the workpiece in the technical solution of the present invention is a cylindrical roller, the cone angles of the spiral groove rolling surface cones of the two guide rollers are equal in size and opposite in direction. The value of the inclination angle α is between 0.5 ° and 2 °.
When the workpiece in the technical solution of the present invention is a tapered roller, the cone angles of the spiral groove rolling surface cones of the two guide rollers are not equal in size and opposite in direction. The value of the inclination angle α is half of the cone angle of the tapered roller plus 0.5 ° to 2 °.
Due to the use of oblique ultra precision technology, the outer diameter of cylindrical rollers and tapered rollers in this invention can obtain a "logarithmic curve" convex shape, which can increase the service life of the product by more than 2-3 times. Due to the presence of a spiral edge on one of the guide rollers, the spiral groove rolling surface of the two guide rollers can be designed as a complementary conical surface, making the manufacturing and processing of the guide rollers easy, the method simple, the process performance stable, and easy to widely promote and apply. This will play a very important role in creating quality and efficiency for enterprises.
The illustration of the attached diagram is as follows:
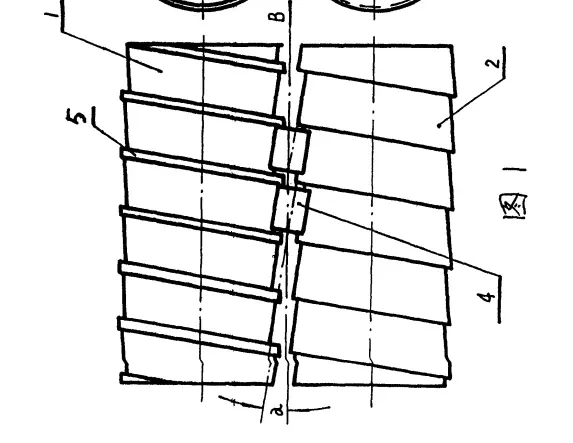
Figure 1 is a schematic diagram of the outer diameter of the ultra precision cylindrical roller of the present invention, and serves as an abstract drawing of the specification;
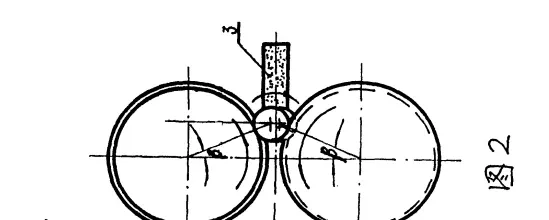
Figure 2 is a schematic diagram from the right side of Figure 1;
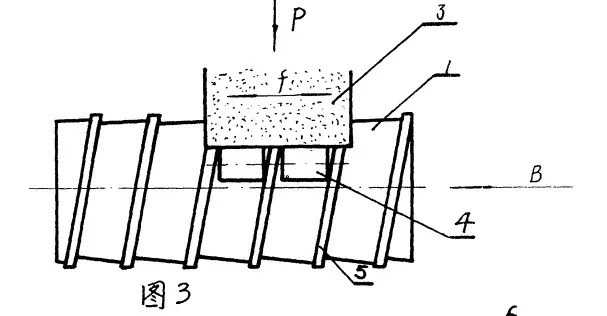
Figure 3 is a schematic bottom view of Figure 1;
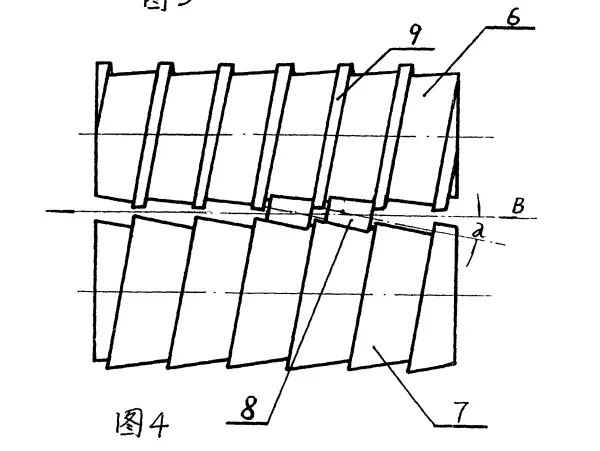
Figure 4 is a schematic diagram of the outer diameter of the ultra precision tapered roller of the present invention;
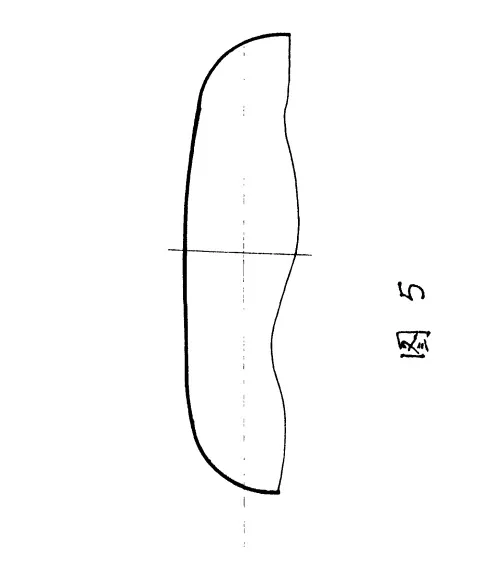
Figure 5 shows the basic shape of the "logarithmic curve" convexity obtained by the ultra precision method of the present invention.
The present invention will be further described in conjunction with the accompanying drawings: Figures 1, 2, and 3 are schematic diagrams of cylindrical roller ultra precision. The device used includes a guide roller 1 with a blocking edge, a guide roller 2 without a blocking edge, and an oilstone group 3. The workpiece 4 is a cylindrical roller. The guide roller 1 is equipped with a spiral edge 5, which plays a role in pushing the workpiece 4 forward. The cone angles of the spiral groove rolling surfaces of guide rollers 1 and 2 are equal in size, opposite in direction, and parallel in axis. The axis of workpiece 4 is inclined to the left or right by an angle of 0.5 ° to 2 ° relative to its advancing direction B. The plane formed by the upper generatrix of workpiece 4 and the axis of guide rollers 1 and 2 is parallel. The diameters of the two guide rollers 1 and 2 are basically equal, and the rotation speed and direction are the same. Under their support and driving, the workpiece 4 rotates on its own while advancing in the direction indicated by B. For each rotation of the guide rollers 1 and 2, the workpiece 4 advances by one pitch. Under the action of the vibration frequency f and pressure P of oil stone group 3, workpiece 4 can obtain a "logarithmic curve" convex shape as shown in Figure 5. The angle β between the center of workpiece 4 and the center line of guide rollers 1 and 2 is generally taken as 12 ° to 18 °.
Figure 4 is a schematic diagram of the super precision of the convexity of the tapered roller. The guide roller 6 is equipped with a spiral retaining edge 9. The difference between guide rollers 6 and 7 and guide rollers 1 and 2 is that the cone angles of their spiral groove rolling surfaces are not equal in size and opposite in direction. The size of the cone angle is determined by the cone angle of the tapered roller. Workpiece 8 is a tapered roller, and the plane formed by the upper generatrix of Workpiece 8 and the axis lines of guide rollers 6 and 7 is parallel. The axis line of Workpiece 8 is inclined to the left or right relative to its advancing direction B, and the taper angle of the tapered roller is half plus an angle of 0.5 ° to 2 °. Under the support and driving of guide rollers 6 and 7, workpiece 8 achieves super precision convexity under the vibration frequency f and pressure P of oilstone group 3, obtaining the "logarithmic curve" outer diameter as shown in Figure 5.
Figure 5 shows the shape of the logarithmic curve of the basic cylindrical and tapered roller generatrix profile. When the value of the inclination angle α changes, the shape of the logarithmic curve also changes slightly.
2024 July 4th Week WBM Product Recommendation:
Heading dies,Punch:
WBM produces taper roller dies with high efficiency and automation. Rollers are formed on a single automatic cold heading press and are fed, cut, and punched into the die for five steps.
We can produce different types and sizes taper roller dies with quality assurance,include:Combination Punch,Outside Sleeve,Blade,Combination Punch,Feed Cylinder,Combination Dies,Double Layer Sleeve,Insert.
https://www.w-bm.com/products/Taper-roller-cold-heading-dies/Heading-dies,Punch/400.html