Abstract
The present invention discloses a production method for a high-speed and high-precision CNC machine tool bearing special steel ball, which adopts the following steps: the steel ball cold heading adopts a sleeve cutting, shaping, and cold heading multi station high-speed cold heading method to process the blank; The rough machining adopts the large cycle photosphere process; Adopting a continuous drum furnace for controllable atmosphere quenching, cold treatment, and tempering treatment, with automatic control of carbon potential; Applying frequency conversion speed regulation with multi plate structure for surface strengthening; Hard grinding adopts ceramic grinding wheel large cycle process for processing; After the initial research, double roll sorting will be adopted; Perform photoelectric eddy current testing after precision research; Perform ultra precision machining after aging treatment; Optoelectronic detection after ultra precision research. The diameter variation of the steel ball processed and produced by the present invention is less than 0.07 μ m, roundness is less than 0.05 μ m, spherical error is less than 0.05 μ m, surface roughness Ra is less than 0.007 μ m, ball batch diameter variation is less than 0.09 μ m, and the dmn value of the bearing after the steel ball is assembled is greater than 2.5 × 106mm · r/min.
Description
Production method of special steel balls for bearings in high-speed and high-precision CNC machine tools
technical field
The present invention relates to a steel ball production method, in particular to a production method for a high-speed and high-precision CNC machine tool bearing special steel ball.
Background technology
At present, the bearings of precision and high-speed CNC machine tools belong to high-precision and high-tech bearing varieties, with high technical content and difficult development. Currently, most of them rely on imports, which seriously restricts the localization process of precision and high-speed CNC machine tools and has become a key component that urgently needs to replace imports. Bearings mainly consist of four parts: steel balls, inner and outer rings, and retainers. Among the four major components of bearings, steel balls are the weakest link, and the surface texture of steel balls directly affects the service life of bearings. The impact rate on bearing vibration and noise is over 60%, and more than 80% of bearing failures are caused by the failure of steel balls.
At present, there is not much difference in the single particle geometric accuracy such as roughness and roundness between China's steel balls and foreign high-precision steel balls through testing. However, there is a significant difference in the vibration and noise values of bearings after fitting. This difference is caused not only by differences in raw materials, but also by differences in heat treatment levels and steel ball forming processes, resulting in different working conditions of steel balls in bearings, which has a significant impact on bearing vibration, noise, and service life.
The traditional production process of steel balls generally adopts processes such as cold heading, light ball, quenching and tempering treatment, hard grinding, initial research, and precision research, but it still cannot meet the requirements of high-speed and high-precision CNC machine tool bearing special steel balls.
summary of the invention
The purpose of the present invention is to overcome the shortcomings of the existing technology and provide a production method for high-speed and high-precision CNC machine tool bearings dedicated steel balls. The method has a simple process and the produced steel balls can meet the requirements of the Technical Conditions for Fine Steel Balls of Rolling Bearings.
To achieve the above objectives, the present invention adopts the following technical solution:
A high-speed and high-precision CNC machine tool bearing specialized steel ball production method, with the following steps:
(1) Steel ball cold heading, using multi station high-speed cold heading method to process blanks;
(2) Rough machining, using large cycle photosphere technology;
(3) Heat treatment, using continuous drum furnace controlled atmosphere quenching, cold treatment, tempering treatment, and automatic control of carbon potential;
(4) Surface strengthening, using frequency conversion speed regulation and multi plate structure for surface strengthening;
(5) Hard grinding, processed using ceramic grinding wheel large cycle technology;
(6) Preliminary research, followed by the use of double roll sorting;
(7) Precision research, followed by photoelectric eddy current testing;
(8) Timely processing followed by ultra precision machining;
(9) Photoelectric inspection, after ultra precision grinding, uses a photoelectric appearance instrument to detect surface defects on the steel ball.
In step (1), the bearing steel wire is first cut into sections using a sleeve cutting method, then the sections are shaped, and finally the sections are upset into steel ball blanks.
In step (2), the machining amount for each car is 1000-1200Kg, and filing and grinding are carried out separately; Firstly, the filing process is adopted to eliminate the ring and polar burrs, and then the grinding process is carried out. The processing speed is 90-130r/min, the pressure is 100-200KN, and the grinding amount is 0.15-0.20mm.
In step (3), a continuous drum furnace nitrogen based controllable atmosphere is used for quenching, and the quenching medium is fast quenching oil. After quenching, cold treatment is carried out, and finally tempering treatment is carried out. The quenching heating temperature is 830-850 ℃, the quenching medium temperature is 60-80 ℃, the cold treatment temperature is 6-8 ℃, and the tempering temperature is 140-160 ℃. The atmosphere is nitrogen+propane+methanol (nitrogen 8-10m3/h, propane 0-300L/h automatic control, methanol 1-2.5L/h).
In step (4), the plate speed is 160-200r/min, the drum speed is 8-12r/min, the surface hardness after strengthening is HRC62-63.5, and then tempering treatment is carried out at a tempering temperature of 140-150 ℃.
The initial grinding in step (6) is carried out on a vertical grinding machine, using a 2000 # resin grinding wheel with a processing speed of 10-30r/min and a pressure of 2-4KN; The double roll sorting adopts the steel ball size inspection method, with the double rolls arranged in an inclined distribution. According to different product specifications, the corresponding distance and inclination angle are adjusted to classify and select qualified products, sizes with larger or smaller specifications.
The precision grinding in step (7) is carried out on a vertical grinding machine, using a 4000 # resin grinding wheel with a processing speed of 10-20r/min and a pressure of 1-3KN; Photoelectric eddy current testing uses three probes, namely photoelectric, eddy current, and vibration, to synchronously detect surface and internal defects of steel balls.
The aging treatment in step (8) adopts a mesh belt furnace for artificial aging, with a temperature of 120-150 ℃, to eliminate residual stress and improve dimensional accuracy; Ultra precision grinding is processed on a vertical grinding machine without adding abrasives. It uses a 6000 # resin grinding wheel and water-based precision grinding fluid, with a processing speed of 10-15r/min and a pressure of 0.8-1KN.
The water-based grinding fluid is used for processing in steps (2) and (5); In steps (6) and (7), diamond micro powder was mixed with aqueous polishing solution (150-500 grams of diamond micro powder were added per kilogram of aqueous polishing solution) as the grinding agent.
The beneficial effects of the present invention are: the diameter variation of the steel ball processed by the present invention is less than 0.07 μ m, the roundness is less than 0.05 μ m, the spherical error is less than 0.05 μ m, the surface roughness Ra is less than 0.007 μ m, the diameter variation of the ball batch is less than 0.09 μ m, and the dmn value of the bearing after the steel ball is assembled is greater than 2.5X106mm · r/min.
The process route adopted by the present invention is based on the existing steel ball processing technology, by analyzing the relevant factors affecting the precision, service life, and high-speed performance index (dmn) of the steel ball, selecting reliable and reasonable process methods and reasonable process equipment to improve the manufacturing accuracy, service life, and high-speed performance of the steel ball
Specific implementation methods
The following will further explain the present invention in conjunction with embodiments.
Example 1: Taking the production process of 3.969mm (5/32) steel balls as an example, the material of the steel balls is GCr15.
Steel ball cold heading: using a sleeve to cut the bearing steel wire on a high-speed cold heading machine; Then shape the material section and remove burrs; Then proceed with cold heading. Adopting a multi station cold heading method, 700 blanks are processed per minute with a size of 4.27mm.
(2) Rough machining
Adopting the large circulation photosphere process and water-based grinding fluid processing, with a processing capacity of 1000Kg, the first step is to use the filing process to eliminate the ring and polar burrs, and then rotate the lathe for grinding processing. Processing speed of 90r/min, pressure of 100KN, grinding amount of 0.18mm.
(3) Heat treatment
Continuous drum furnace is used for nitrogen based controllable atmosphere quenching, with fast quenching oil as the quenching medium. After quenching, it undergoes cold treatment and finally tempering treatment. Quenching heating temperature of 830 ℃, quenching medium temperature of 70 ℃, cold treatment temperature of 7 ℃, tempering temperature of 160 ℃, atmosphere of nitrogen+propane+methanol (nitrogen 8m3/h, propane 0-300L/h automatic control, methanol 2L/h), quenching cold treatment tempering production line.
(4) Surface strengthening
Applying variable frequency speed regulation with multi plate structure for surface strengthening, the plate speed is 160r/min, the drum speed is 8r/min, and the surface hardness after strengthening is HRC62-63.5. Then carry out tempering treatment, with a tempering temperature of 140 ℃.
(5) Hard grinding
Hard grinding adopts ceramic grinding wheel large cycle technology, processed with water-based grinding fluid, with a grinding amount of 0.09mm.
(6) Preliminary research
Preliminary grinding is carried out on a vertical grinding machine, using a mixture of diamond micro powder and water-based precision grinding fluid as grinding agent (150 grams of diamond micro powder per kilogram of water-based precision grinding fluid), 2000 # resin grinding wheel, processing speed of 15r/min, and pressure of 2KN.
(7) Double roll sorting
The double roll sorting adopts the steel ball size inspection method, with the double rolls arranged in an inclined distribution. Qualified products, sizes with larger or smaller values are classified and selected.
(8) Precision research
Preliminary grinding is carried out on a vertical grinding machine, using a mixture of diamond micro powder and water-based precision grinding fluid as grinding agent (150 grams of diamond micro powder per kilogram of water-based precision grinding fluid), 4000 # resin grinding wheel, processing speed of 15r/min, and pressure of 1KN.
(9) Photoelectric eddy current testing
Synchronous detection of surface and internal defects of steel balls using three probes: photoelectric, eddy current, and vibration.
(10) Timely processing
Using a mesh belt tempering furnace for artificial aging at a temperature of 120 ℃ to eliminate residual stress and improve dimensional accuracy.
(11) Ultra precision research
Perform preliminary grinding on a vertical grinding machine without adding abrasive, using 6000 # resin grinding wheel and water-based precision grinding fluid. Processing speed of 10r/min, pressure of 0.8KN.
(12) Optoelectronic inspection
Using a photoelectric appearance meter to detect surface defects on steel balls.
Example 2: Taking the production process of 5.953mm (15/64) steel balls as an example, the material of the steel balls is GCr15.
Steel ball cold heading: using a sleeve to cut the bearing steel wire on a high-speed cold heading machine; Then shape the material section and remove burrs; Then proceed with cold heading. Adopting multi station cold heading method, processing 600 blanks per minute, with blank size
(2) Rough machining
Adopting the large circulation photosphere process and water-based grinding fluid processing, with a processing capacity of 1100Kg, the first step is to use the filing process to eliminate the ring and polar burrs, and then rotate the lathe for grinding processing. Processing speed 130r/min, pressure 150KN, grinding amount 0.15mm.
Heat treatment
Continuous drum furnace is used for nitrogen based controllable atmosphere quenching, with fast quenching oil as the quenching medium. After quenching, it undergoes cold treatment and finally tempering treatment. Quenching heating temperature 845 ℃, quenching medium temperature 60 ℃, cold treatment temperature 8 ℃, tempering temperature 140 ℃, atmosphere of nitrogen+propane+methanol (nitrogen 9m3/h, propane 0-300L/h automatic control, methanol 1L/h), quenching cold treatment tempering production line.
(4) Surface strengthening
Applying variable frequency speed regulation with multi plate structure for surface strengthening, the plate speed is 180r/min, the drum speed is 10r/min, and the surface hardness after strengthening is HRC62-63.5. Then carry out tempering treatment, with a tempering temperature of 140 ℃.
(5) Hard grinding
Hard grinding adopts ceramic grinding wheel large cycle technology, processed with water-based grinding fluid, with a grinding amount of 0.09mm.
(6) Preliminary research
Preliminary grinding is carried out on a vertical grinding machine, using a mixture of diamond micro powder and water-based precision grinding fluid as grinding agent (400 grams of diamond micro powder per kilogram of water-based precision grinding fluid), 2000 # resin grinding wheel, processing speed of 25r/min, and pressure of 3KN.
(7) Double roll sorting
The double roll sorting adopts the steel ball size inspection method, with the double rolls arranged in an inclined distribution. Qualified products, sizes with larger or smaller values are classified and selected.
(8) Precision research
Preliminary grinding is carried out on a vertical grinding machine, using a mixture of diamond micro powder and water-based precision grinding fluid as grinding agent (200 grams of diamond micro powder per kilogram of water-based precision grinding fluid), 4000 # resin grinding wheel, processing speed of 15r/min, and pressure of 2.5KN.
(9) Photoelectric eddy current testing
Synchronous detection of surface and internal defects of steel balls using three probes: photoelectric, eddy current, and vibration.
(10) Timely processing
Using a mesh belt tempering furnace for artificial aging at a temperature of 135 ℃ to eliminate residual stress and improve dimensional accuracy.
(11) Ultra precision research
Perform preliminary grinding on a vertical grinding machine without adding abrasive, using 6000 # resin grinding wheel and water-based precision grinding fluid. Processing speed of 12r/min, pressure of 0.9KN.
(12) Optoelectronic inspection
Using a photoelectric appearance meter to detect surface defects on steel balls.
Example 3: Taking the production process of 6.747mm (17/64) steel balls as an example, the material of the steel balls is GCr15.
(1) Steel ball cold heading: using a sleeve to cut the bearing steel wire on a high-speed cold heading machine; Then shape the material section and remove burrs; Then proceed with cold heading. Adopting multi station cold heading method, processing 600 blanks per minute, with blank size.
(2) Rough machining
Adopting the large circulation photosphere process and water-based grinding fluid processing, with a processing capacity of 1200Kg, the first step is to use the filing process to eliminate the ring and polar burrs, and then rotate the lathe for grinding processing. Processing speed of 110r/min, pressure of 200KN, grinding amount of 0.20mm.
(3) Heat treatment
Continuous drum furnace is used for nitrogen based controllable atmosphere quenching, with fast quenching oil as the quenching medium. After quenching, it undergoes cold treatment and finally tempering treatment. Quenching heating temperature of 850 ℃, quenching medium temperature of 80 ℃, cold treatment temperature of 6 ℃, tempering temperature of 150 ℃, atmosphere of nitrogen+propane+methanol (nitrogen 10m3/h, propane 0-300L/h automatic control, methanol 2.5L/h), quenching cold treatment tempering production line.
(4) Surface strengthening
Applying variable frequency speed regulation with multi plate structure for surface strengthening, the plate speed is 200r/min, the drum speed is 12r/min, and the surface hardness after strengthening is HRC62-63.5. Then carry out tempering treatment, with a tempering temperature of 150 ℃.
(5) Hard grinding
Hard grinding adopts ceramic grinding wheel large cycle technology, processed with water-based grinding fluid, with a grinding amount of 0.09mm.
(6) Preliminary research
Preliminary grinding is carried out on a vertical grinding machine, using a mixture of diamond micro powder and water-based precision grinding fluid as grinding agent (500 grams of diamond micro powder per kilogram of water-based precision grinding fluid), 2000 # resin grinding wheel, processing speed, 30r/min, and pressure of 4KN.
(7) Double roll sorting
The double roll sorting adopts the steel ball size inspection method, with the double rolls arranged in an inclined distribution. Qualified products, sizes with larger or smaller values are classified and selected.
(8) Precision research
Preliminary grinding is carried out on a vertical grinding machine, using a mixture of diamond micro powder and water-based precision grinding fluid as grinding agent (500 grams of diamond micro powder per kilogram of water-based precision grinding fluid), 4000 # resin grinding wheel, processing speed of 20r/min, and pressure of 3KN.
(9) Photoelectric eddy current testing
Synchronous detection of surface and internal defects of steel balls using three probes: photoelectric, eddy current, and vibration.
(10) Timely processing
Using a mesh belt tempering furnace for artificial aging at a temperature of 150 ℃ to eliminate residual stress and improve dimensional accuracy.
(11) Ultra precision research
Perform preliminary grinding on a vertical grinding machine without adding abrasive, using 6000 # resin grinding wheel and water-based precision grinding fluid. Processing speed of 10r/min, pressure of 1KN.
(12) Optoelectronic inspection
Using a photoelectric appearance meter to detect surface defects on steel balls.
2024 July 1st Week WBM Product Recommendation:
Steel Ball Cold Heading Tools:
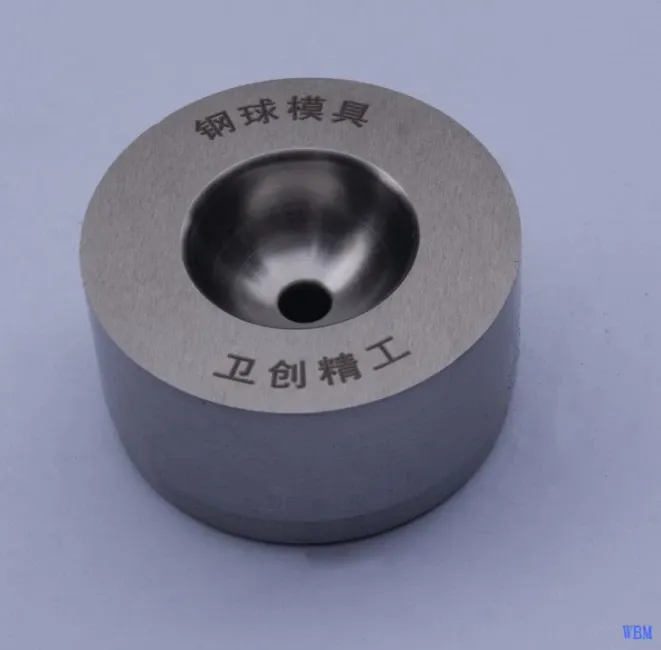
n the steel ball cold heading process, after barstocks are cut into column-shaped blanks, two ends of the column shaped blanks are rubbed and cut into inversed angel or round angle shapes, and then the blanks are transferred to a cold heading mechanism to be headed into steel ball rough cast; a blank rubbing and cutting mechanism is additionally arranged on the corresponding cold heading machine. The quality and eligibility rate of the steel ball rough cast can be enhanced and the manufacturing cost thereof can be reduced. Furthermore, as the shapes of the blanks entering the cold forging mechanism are regular, the stress born by the cold heading mechanism is equal in the punching process, thus the service life of cold heading dies is prolonged.