Abstract
The present invention discloses a method for processing the cavity of a roller punch using cold extrusion technology. The method involves making an extrusion punch and a positioning sleeve that is adapted to the diameter of the punch according to the forming size of the roller punch. The cold extrusion punch and the roller punch blank are placed in the positioning sleeve, and the forming part of the extrusion punch is pressed into the punch blank using a hydraulic press. After pressing to the desired depth, the extrusion punch and the punch blank can be released by unloading the pressure. Compared with existing methods for turning roller punches, the present invention has the following characteristics: (1) the size accuracy of the extruded punch can reach 8-9 levels, and the surface roughness can reach Ra0.4 μ m. (2) The squeezing punch technology has low difficulty and high production efficiency. (3) The size consistency of the extruded punch is good. (4) Extrusion processing does not cut off the forging flow line of the material. (5) Squeezing processing can weld the looseness inside the material, increase the density of the material, and ultimately improve the strength of the material.
Description
Method of processing roller punch cavity using cold extrusion technology
technical field
The present invention belongs to a method for processing a roller punch, mainly involving a method for processing the cavity of a roller punch using cold extrusion technology.
Background technology
Roller punch is one of the main fixtures for cold heading rollers. At present, roller punch heads are all formed by turning processing, which mainly has the following drawbacks: (1) there are turning tool lines with a roughness of Ra3.2 μ m, which cannot meet the requirements of the drawing. In use, the tool lines can cause stress concentration, leading to punch block failure. (2) The closer the punch is to the center, the lower the cutting speed. In theory, the metal is torn down at the lower cutting speed, resulting in the presence of micro cracks. For the roller punch, the area near the center is where the maximum force per unit area is exerted, and this micro crack will become the trigger for the failure of the roller punch. (3) The technical difficulty and labor intensity of turning punch heads are relatively high, and the production efficiency is low. (4) The punch produced by turning has a relatively scattered hole diameter and poor consistency in size. (5) Turning machining cuts off the original forging flow line of the punch, which to some extent reduces the service life of the punch.
summary of the invention
The purpose of the present invention is to propose a method for processing the cavity of a roller punch using cold extrusion technology, which can not only improve the service life, production efficiency, and dimensional consistency of the punch, but also reduce the difficulty of punch processing.
The purpose of the present invention can be achieved by the following technical solution: making an extrusion punch and a sleeve that is compatible with the outer dimensions of the punch according to the forming size of the roller punch, placing the cold extrusion punch and the roller punch blank into the positioning sleeve, using a hydraulic press to press the forming part of the extrusion punch into the punch blank, and after pressing to the desired depth, releasing the pressure and exiting the extrusion punch and punch blank.
Compared with existing methods for turning roller punches, the present invention has the following characteristics: (1) the size accuracy of the extruded punch can reach 8-9 levels, and the surface roughness can reach Ra0.4 μ m. (2) The squeezing punch technology has low difficulty and high production efficiency. (3) The size consistency of the extruded punch is good. (4) Extrusion processing does not cut off the forging flow line of the material. (5) Squeezing processing can weld the looseness inside the material, increase the density of the material, and ultimately improve the strength of the material.
Attached image description
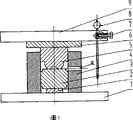
Figure 1 shows the working schematic of the invention.
In the picture: 1. Lower worktable of hydraulic press, 2. Lower pad, 3. Punch blank, 4. Positioning sleeve, 5. Squeezing punch, 6. Upper pad, 7. Tightening screw, 8. Dial gauge, 9. Upper worktable.
Specific implementation method
Describe specific embodiments of the present invention in conjunction with the accompanying drawings.
As shown in Figure 1, first make an extrusion punch 5 according to the forming size of the roller punch, and at the same time make a positioning sleeve 4 that is suitable for the punch diameter. Place the sleeve 4 on the lower worktable 1 of the hydraulic press, place the cold extrusion punch 5 and the roller punch blank 3 into the positioning sleeve 4, place a cushion plate 2 at the lower part of the roller punch blank 3, and also place a cushion plate 6 at the upper part of the extrusion punch 5. Then, the upper worktable 9 of the hydraulic press presses the forming part of the extrusion punch into the roller punch blank, and after pressing to the desired depth, release the pressure and exit the extrusion punch and punch blank. Enter the extruded roller punch blank into the subsequent heat treatment process.
When processing the roller punch blank, a step with a width of 10-15mm is set (turned) on the upper and lower ends of the roller punch blank to relieve pressure and facilitate unloading, and a vent hole 10 is set on the sleeve wall. At the same time, in order to maintain machining accuracy, the gap between the extrusion punch 5 and the positioning sleeve 4 is 0.01-0.02mm, and the gap between the roller punch blank and the positioning sleeve is 0.02-0.04mm.
In order to facilitate the measurement of extrusion depth and ensure safe production during the processing of roller punches, a dial gauge 8 with an extended measuring head is installed on the press, which is fixed to the upper worktable 9 of the press with a clamping screw 7.
2024 November 2th Week WBM Product Recommendation:
Interroll Tapered Roller:
Interroll Tapered Roller is a major products of Henan Weichuang Bearing Precision Technology Co.,Ltd.(WBM). If you need more details, please click the website to know more.
https://www.bearingroller.com/rolling-elements/interroll-2tapered-roller.html