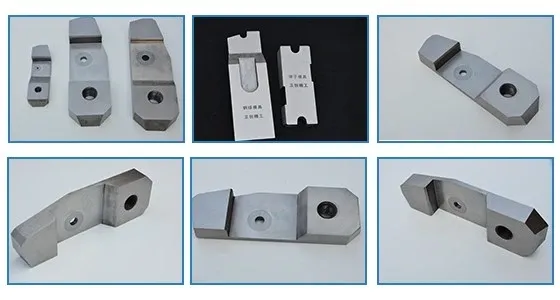
Abstract: The efficiency of batch processing of small knife boards is relatively low. Design a fixture to improve the processing efficiency and accuracy of small knife boards.
Keywords: positioning sales; The principle of leverage; degree of freedom
Preface
1. Introduction
The small cutting edge refers to the cutting edge of the fully automatic bearing special riveting machine, which is processed using a CNC wire cutting machine. Due to the fact that the machining process of CNC machine tools is a single machine operation, the efficiency is relatively low during batch machining. So how to improve the processing efficiency and accuracy of small knife plates is a new problem that arises in the actual processing process.
2. Overview of Small Knife Plate Structure
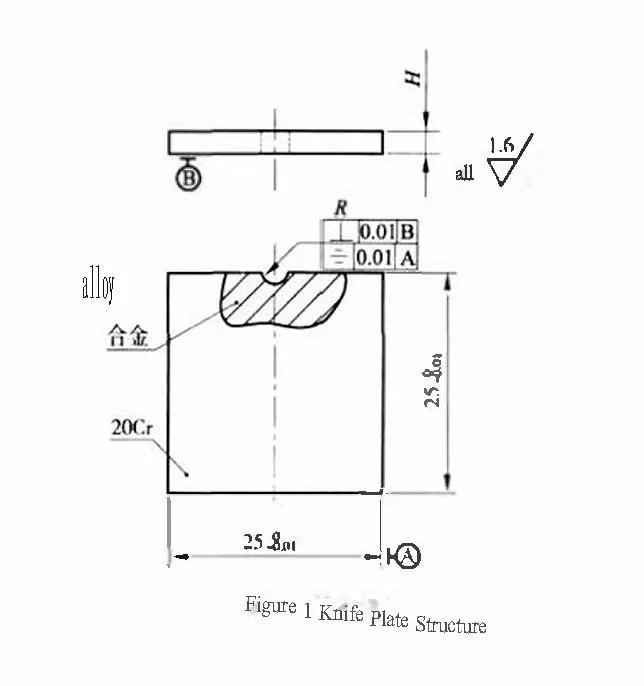
The important cutting component of the fully automatic riveting machine Z is the small blade. Due to the high-speed cutting of the rivet wire by the cutting blade, it is necessary to ensure that the geometric circle at the cutting edge of the rivet remains unchanged, without leaving any scratches or cutting marks. The small knife board has a simple structure, long service life, and stable cutting quality. The structure of the knife plate is shown in Figure 1, with a regular semi-circular blade edge. The circular blade edge is symmetrical on the knife plate, ensuring positional accuracy in the symmetrical axial direction. The consumption of small blade edges is high. The cutting edge is made of hard alloy, while the cutting plate is made of unhardened 20Cr steel, suitable for digital controlled high-speed wire cutting machine processing.
3. Requirements for tooling position and precision position
(1) Ensure that the axis of the small blade edge is perpendicular to the reference plane (large plane) by 0.01mm.
(2) The circular blade edge is ensured to be symmetrical on the cutting plate, with a symmetry value of 0.01mm.
(3) Ensure the positional accuracy of the axis of the small blade edge on the blade.
4. Fixture design
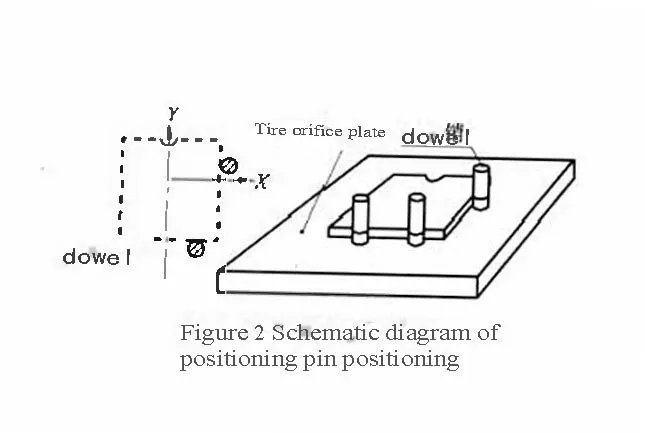
The tire hole plate used in the fixture must ensure that the parallel difference between the two ends of the processed plane is within 0.02mm, and the perpendicularity of the molybdenum wire should be less than 0.3% to ensure the perpendicularity of the axis of the small cutting edge and the reference plane (large plane). According to the machining drawings, positioning pins are used for positioning. Two positioning pins are used for the bottom surface of the small knife plate, and one positioning pin is used for the right surface. Combined with the plane positioning of the tire hole plate, the degrees of freedom of the small knife plate in the X, Y, and Z directions are limited, as shown in Figure 2. After Z, the machining of the positioning pin hole is carried out with (0,0) as the program origin, and at the same time, the machining is small.
The origin of the main program of the knife board also coincides with (0,0), which ensures the accuracy of the positioning pin hole position and also ensures the accuracy of the positioning of the small knife board. As for the symmetry of the small blade and the positional accuracy of the cutting edge, it is ensured by the accuracy of the machine tool itself.
Due to the need to ensure that the small cutting plate is completely against the positioning pin during processing, the small cutting plate needs to be clamped in both X and Y directions, relying on the lever principle for clamping to ensure the clamping position. The designed tooling is shown in Figure 3.
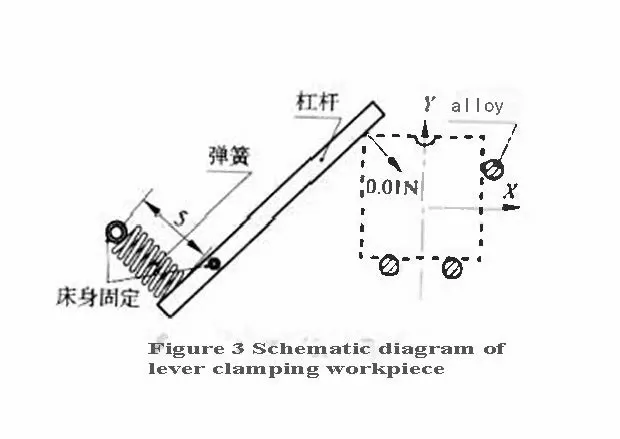
The lever force is on the angular bisector of the coordinate system XOY, ensuring clamping force in the X and Y directions.
Selection and fit error of pins: Steel pins with good rigidity and roundness should be ground after quenching. The fit between the pins and holes should be a smaller degree of interference fit, with a diameter of Φ Taking the 4mm standard cylindrical pin as an example, the tolerance of the pin is the interference fit Z of the cut hole, which is 0.01mm. It should be noted that when cutting the tire hole plate, the interference should not be too large to prevent vibration of the tire hole plate during insertion of the pin, causing loss of reference.
The clamping force of the lever is applied at the corner of the small knife plate, so that the force is evenly distributed along the 135 ° direction. The force needs to make the small knife plate accurately lean against the positioning pin. The long end of the lever is located on the side of the small blade. After setting, the force in the X and Y directions is about 0.007N, and the length ratio of the lever is 4:1. The force at the long end is 0.01N, and the force at the short end is 0.04N. After selecting a spring with an elastic coefficient of 4, only 1cm of travel is needed to achieve the selected force. The distance between the small end and the spring pin is 5cm, and the spring length is selected as 4cm.
5. Conclusion
After the assembly of the tooling is completed, the small knife plate is clamped and processed with a wire cutting machine. The first piece is successful.
After passing the first piece trial cutting inspection, a large batch of small blade processing was carried out, and after inspection, it was proven that this method is completely feasible.
2024 March 4th Week WBM Product Recommendation:
Cutter:
WBM produces taper roller dies with high efficiency and automation. Rollers are formed on a single automatic cold heading press and are fed, cut, and punched into the die for five steps.
We can produce different types and sizes taper roller dies with quality assurance,include:Combination Punch,Outside Sleeve,Blade,Combination Punch,Feed Cylinder,Combination Dies,Double Layer Sleeve,Insert.